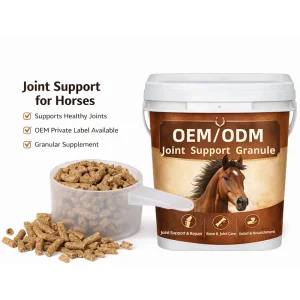
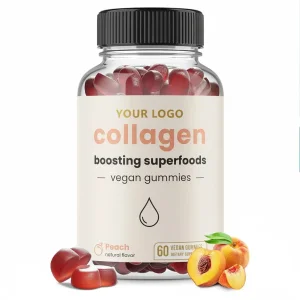
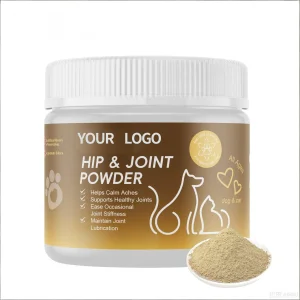
Explore our core certified raw materials and consumer-ready custom formulations engineered for maximum efficacy and bio-absorption.
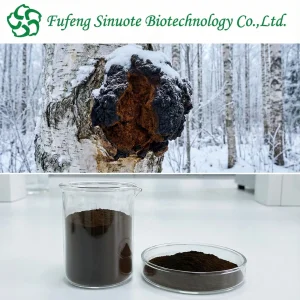
The global dietary supplement market is undergoing a structural transition. Consumer focus has shifted from synthetic micro-nutrients to clean-label, organic, and traceably sourced bioactives. According to current industrial studies, the global organic supplement sector is projected to expand at a CAGR of 8.6% through 2030, driven by strict requirements for allergen-free, vegan-compliant, and non-GMO configurations.
Functional standardization is the baseline. As a custom OEM organic supplements exporter, we address the critical demand for botanical integrity. Modern buyers prioritize dual-extraction processes (e.g., dual-extracted Chaga polysaccharides and triterpenes) and clean-label carriers that do not dilute the efficacy of active ingredients. Synthetic binders are rapidly being replaced by plant-derived fibers and organic starches.
Brands now require more than standard packaging. Our service model provides end-to-end integration: from raw ingredient cultivation monitoring and advanced laboratory analysis to complex multi-ingredient blending. This systematic approach ensures that brands entering markets in the US, EU, or APAC meet local compliance limits for pesticides, heavy metals, and micro-contaminants.
Guangdong Eik Health Co., Ltd. is a specialized, China-based contract manufacturer providing scalable OEM and ODM nutritional supplement solutions. Backed by decadal experience in dietary science, functional food design, and global logistics optimization, we serve as the foundational backbone for leading wellness brands across North America, Europe, and Asia-Pacific.
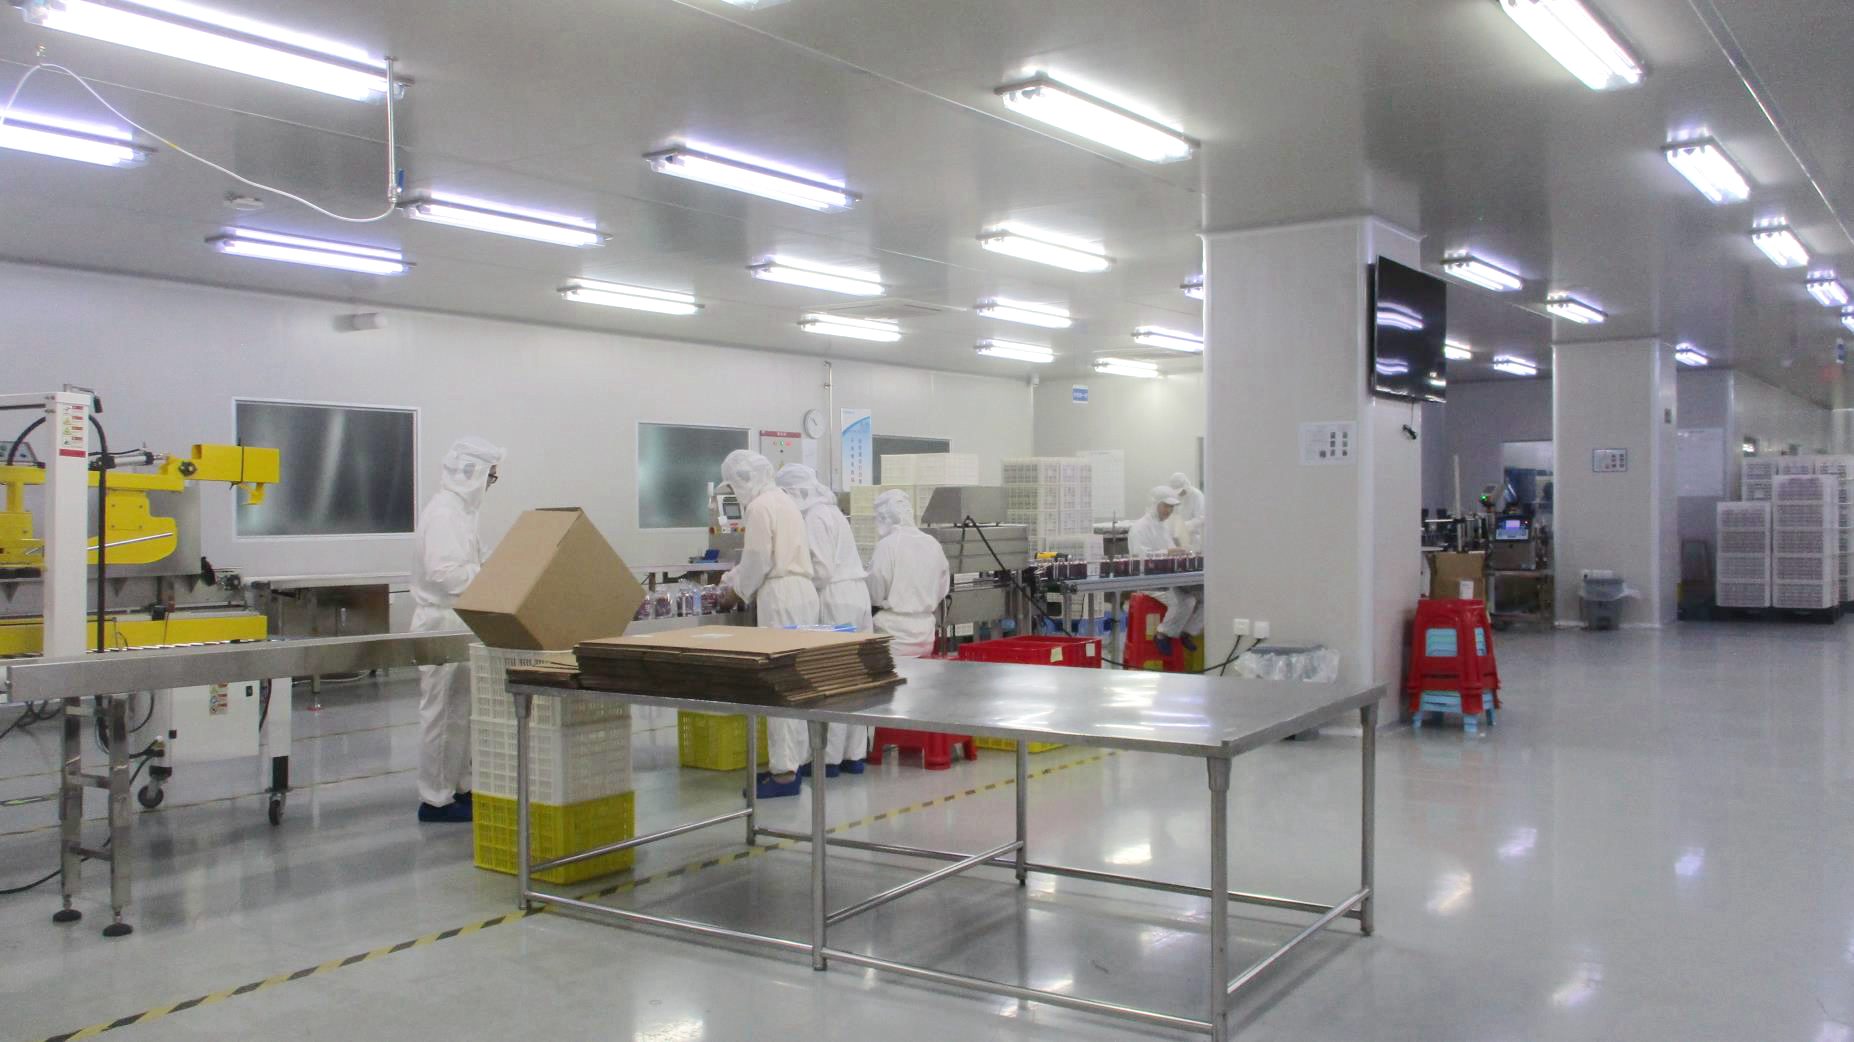
We provide comprehensive, turn-key solutions spanning all phases of product execution: custom formulation engineering, certified raw material sourcing, sensory profiling, regulatory verification, pilot batching, commercial scale-up, and clean-room packaging. Our advanced manufacturing facility accommodates a broad spectrum of delivery formats, including pectin and gelatin-based functional gummies, vegetable-grade hard-shell capsules, softgels, micro-tablets, clean-label powders, unit-dose liquid sachets, and stick-packs. This versatility helps wellness brands quickly bring their concepts to market with retail-ready solutions.
At the center of our operational model is an uncompromised commitment to product safety and regulatory transparency. Our production lines operate under strict GMP/cGMP protocols and hold certifications including HACCP, ISO 22000, and organic processing validation. Each batch undergoes rigorous testing using advanced instrumentation (including HPLC, ICP-MS, and GC-MS) to guarantee active ingredient potency, confirm compound identity, and verify the absence of heavy metals, pesticide residues, and microbial pathogens. This level of quality control ensures our clients can confidently launch products that meet the highest international safety standards.
Our research and development team actively monitors emerging nutritional sciences, giving clients access to over 1,000 functional ingredients, bio-standardized botanicals, clean-label sweeteners, and mineral chelates. We maintain strategic supplier networks that enable us to secure certified organic and wild-harvested raw inputs. Combined with our automated production lines, this supply chain integration allows us to offer flexible production scales, rapid 24-to-48-hour formulation analysis, and quick turnaround times starting at 15 days. We help brands respond dynamically to fluctuating consumer demand and shifting market trends.
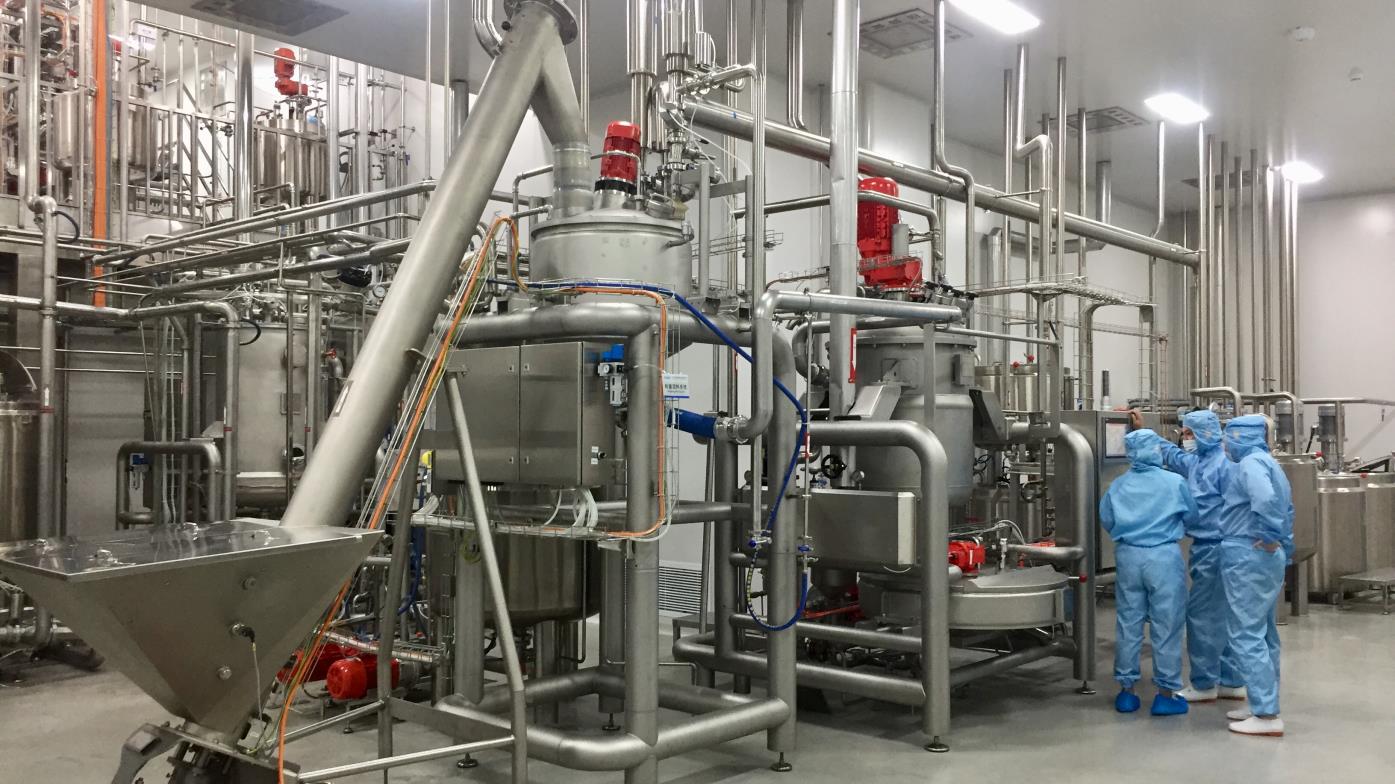
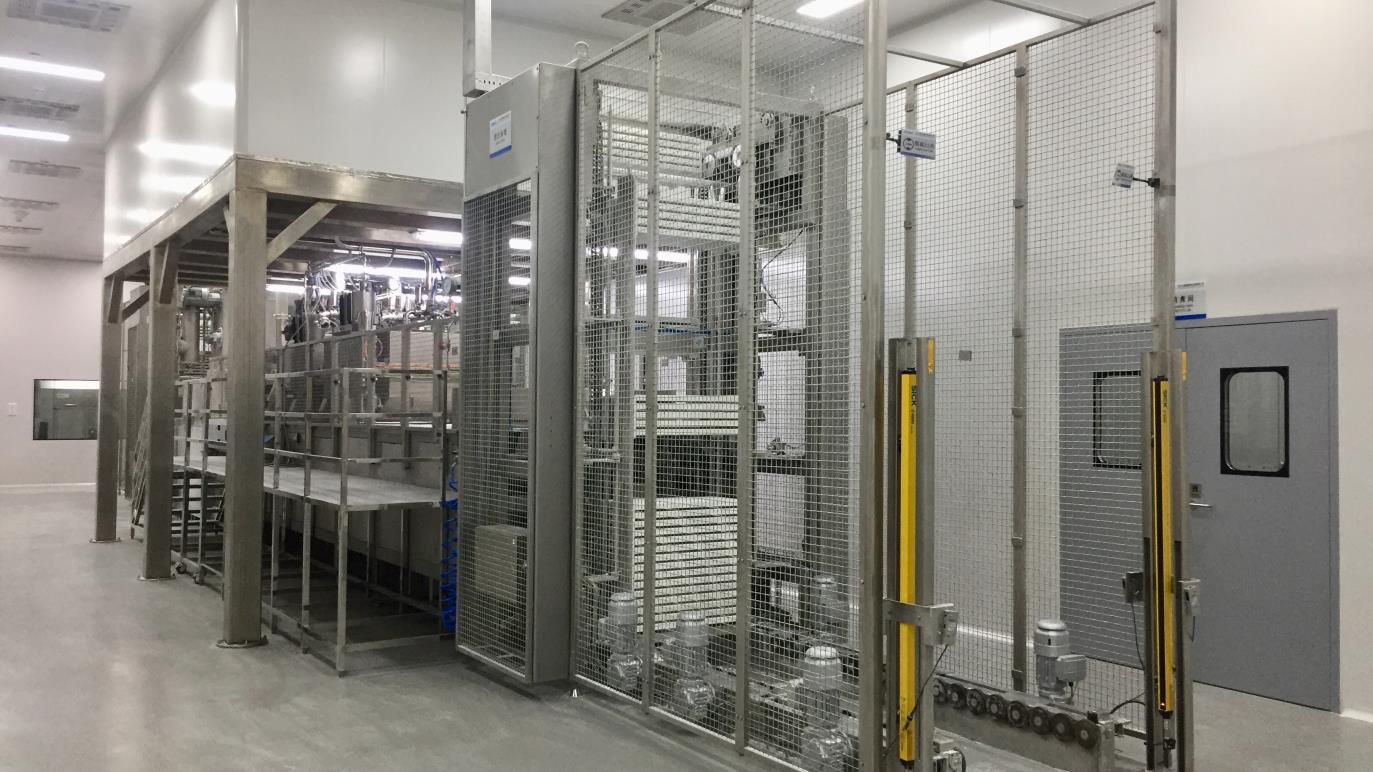
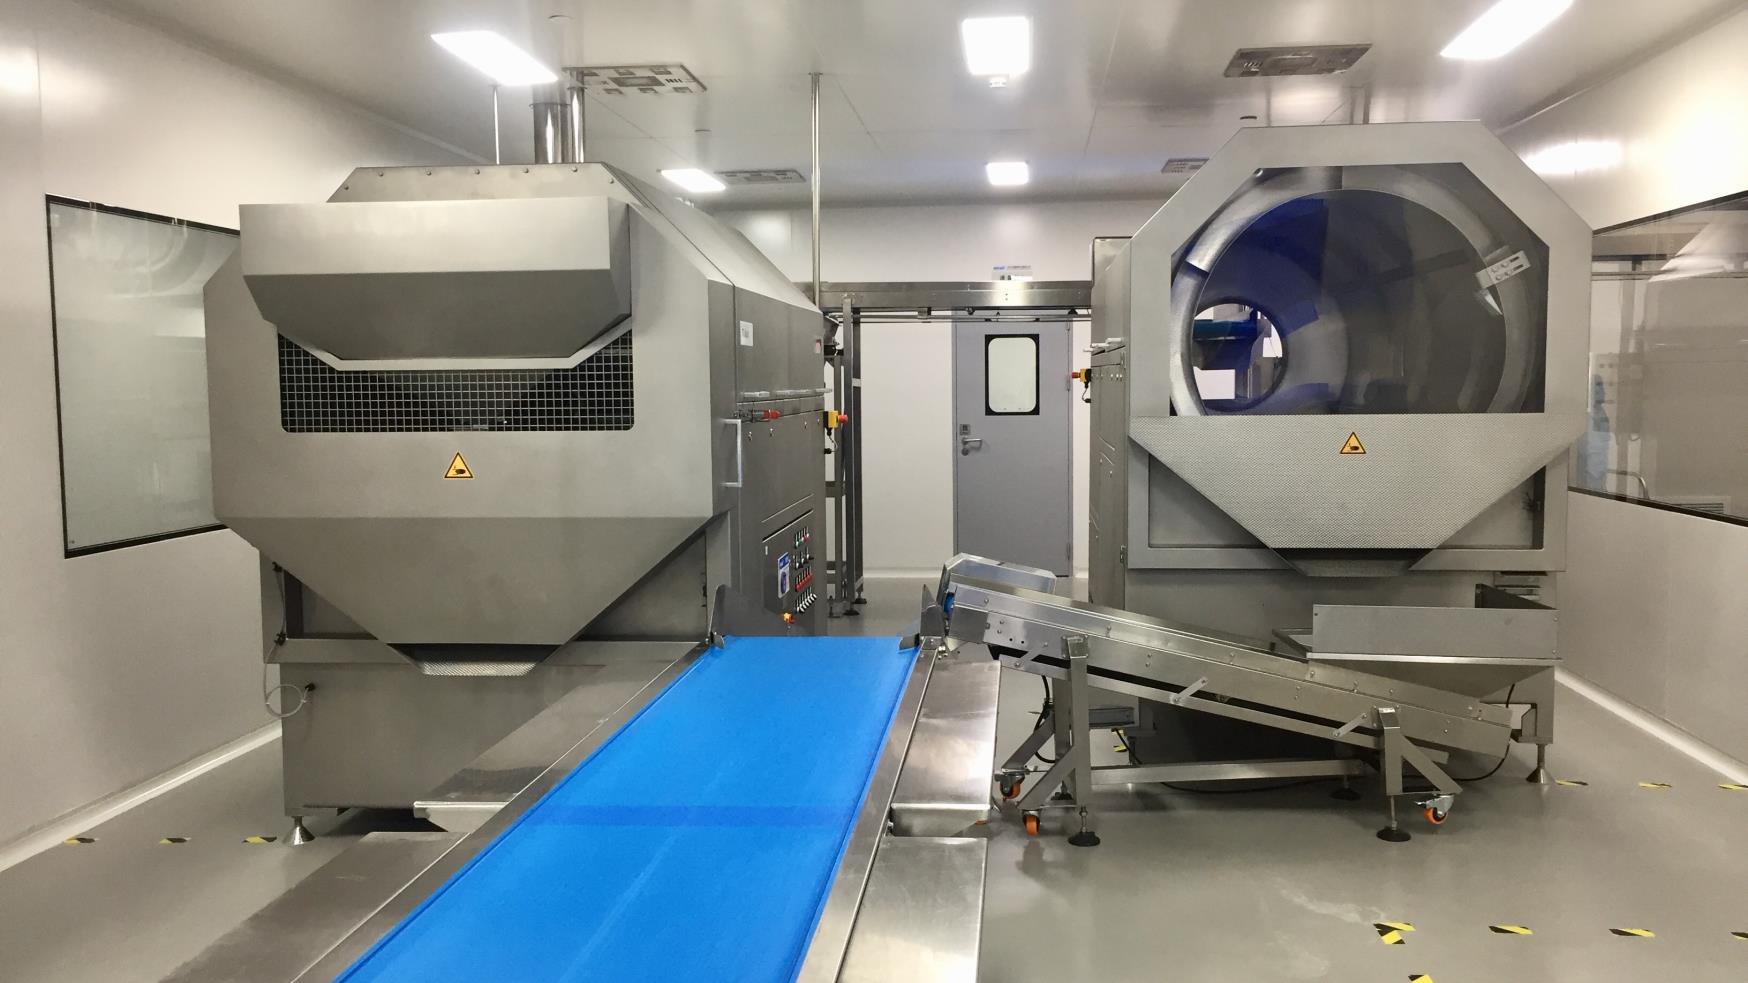
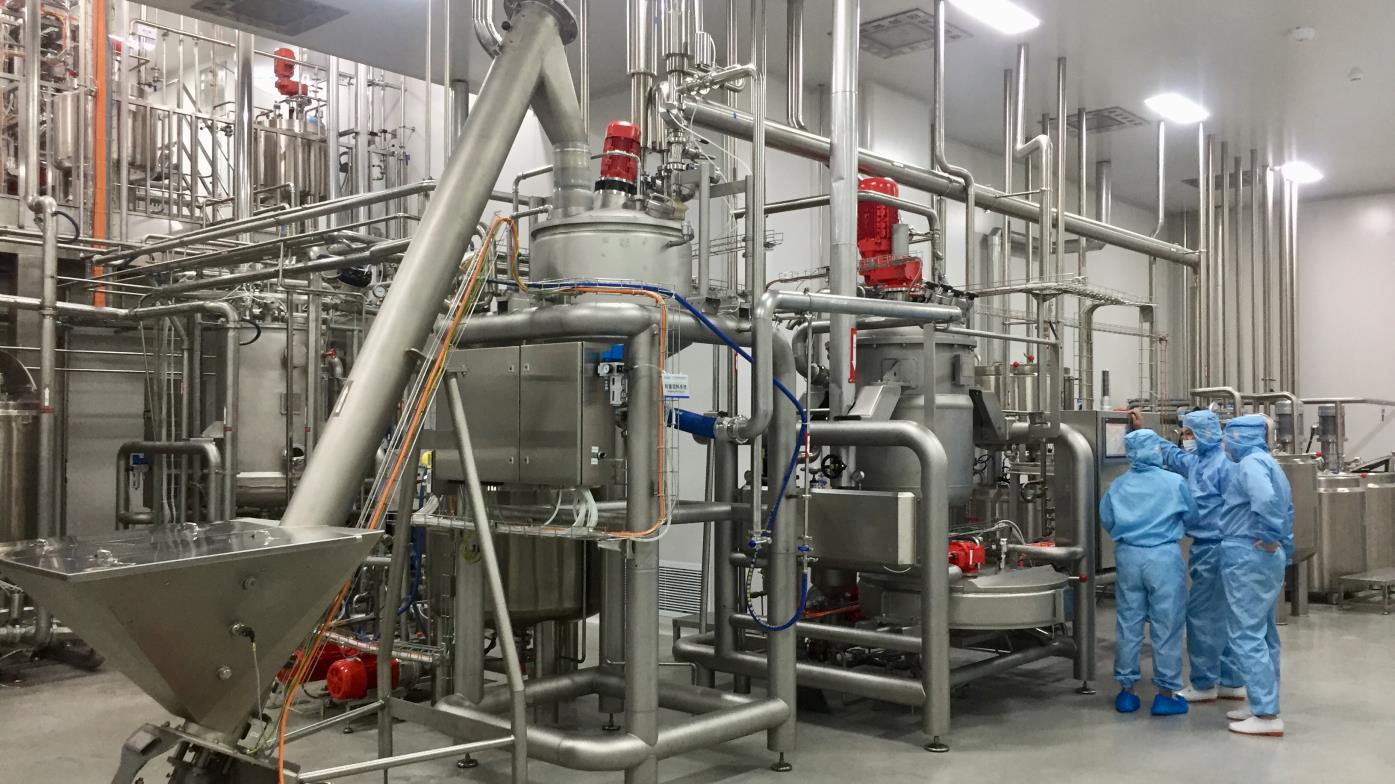
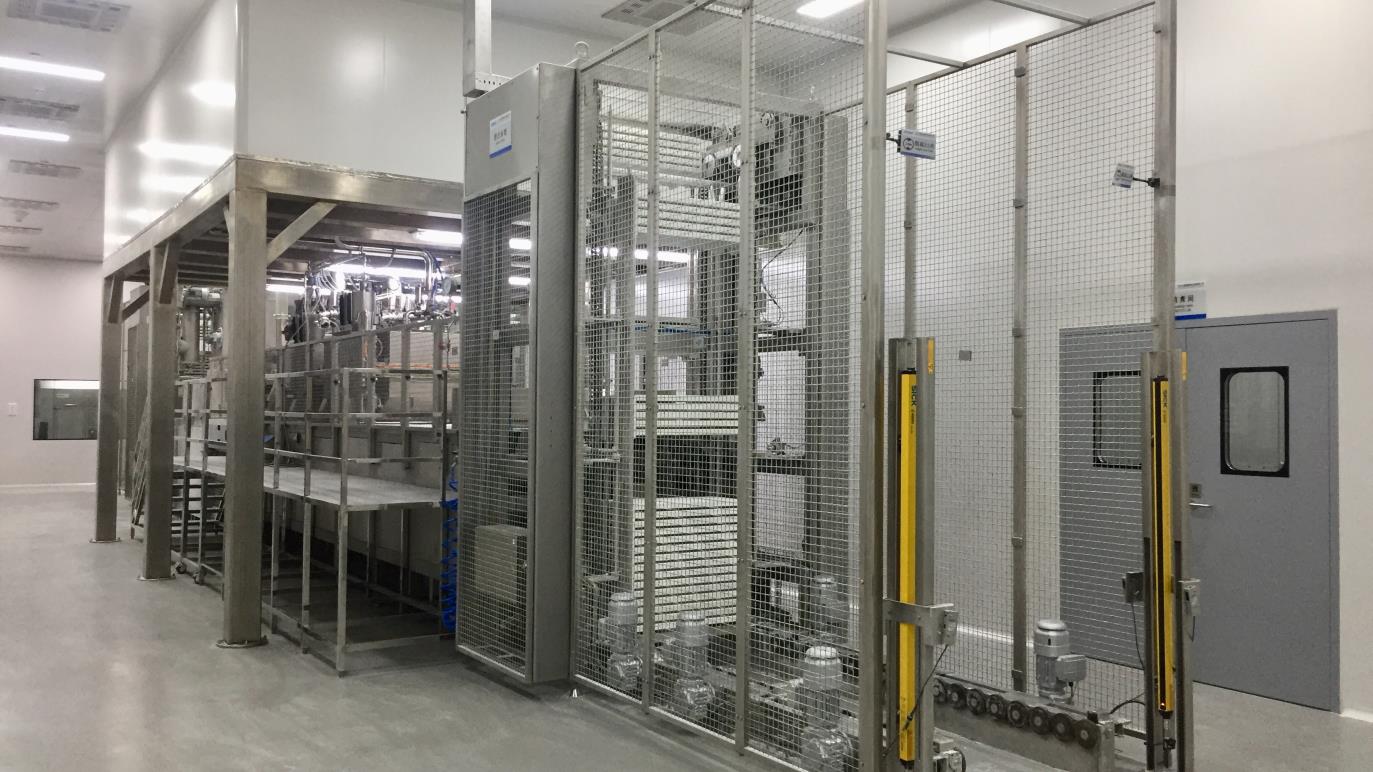
Our production workflow is designed for maximum purity, precision dosing, and absolute process control from raw material preparation to final export packaging.
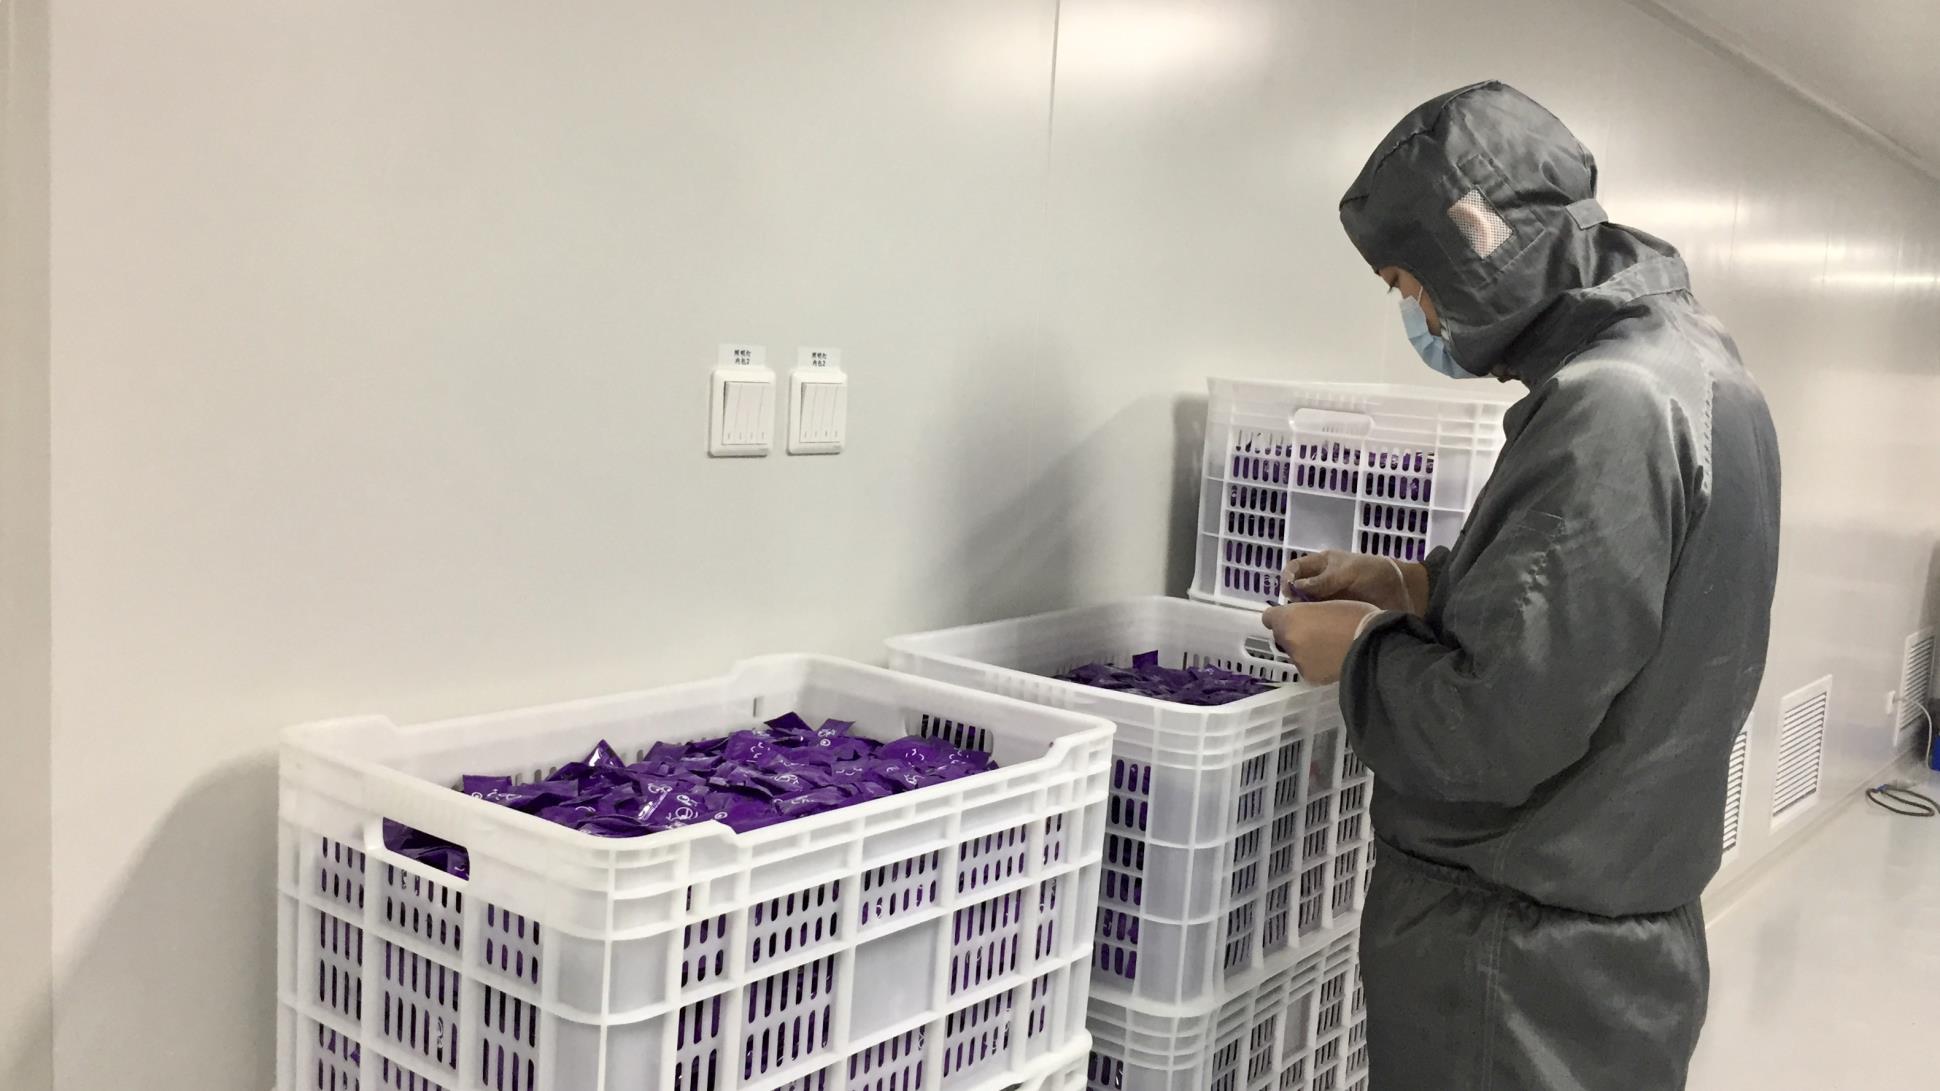
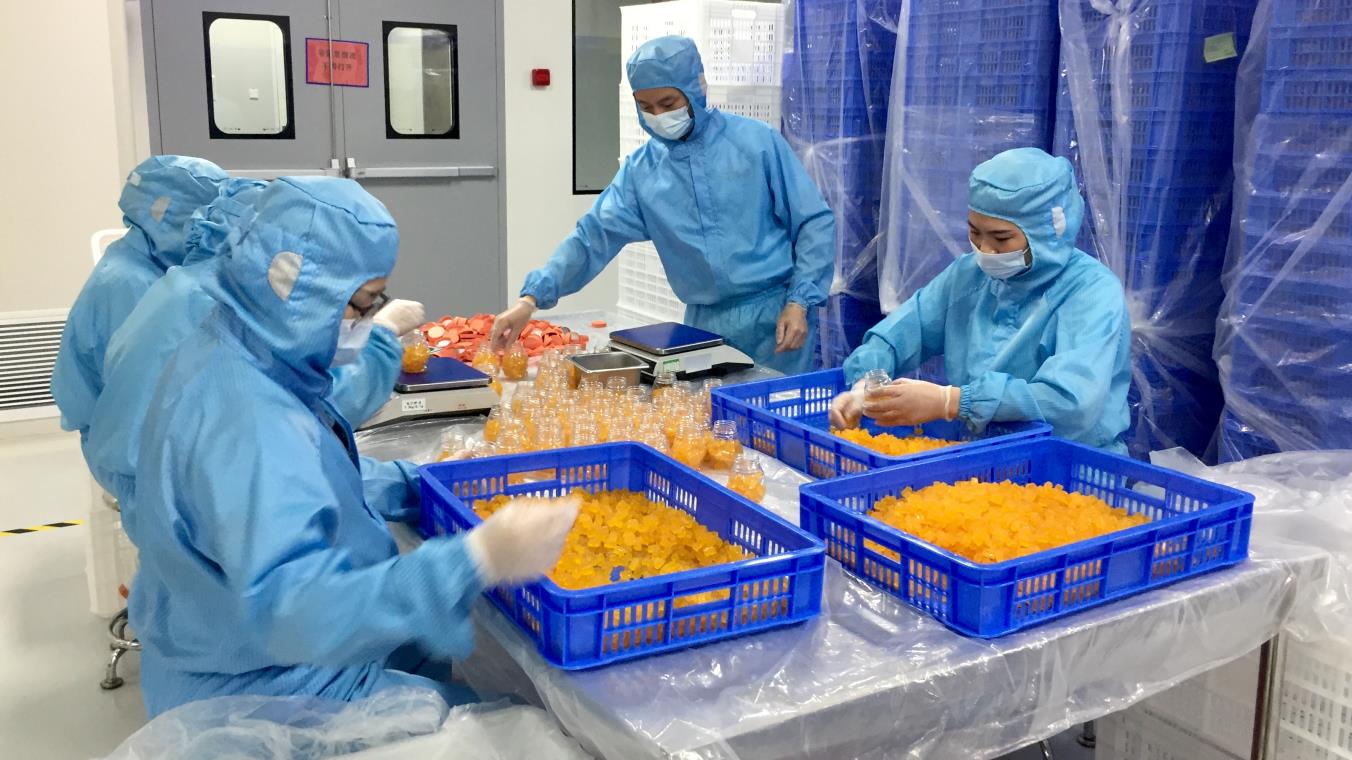
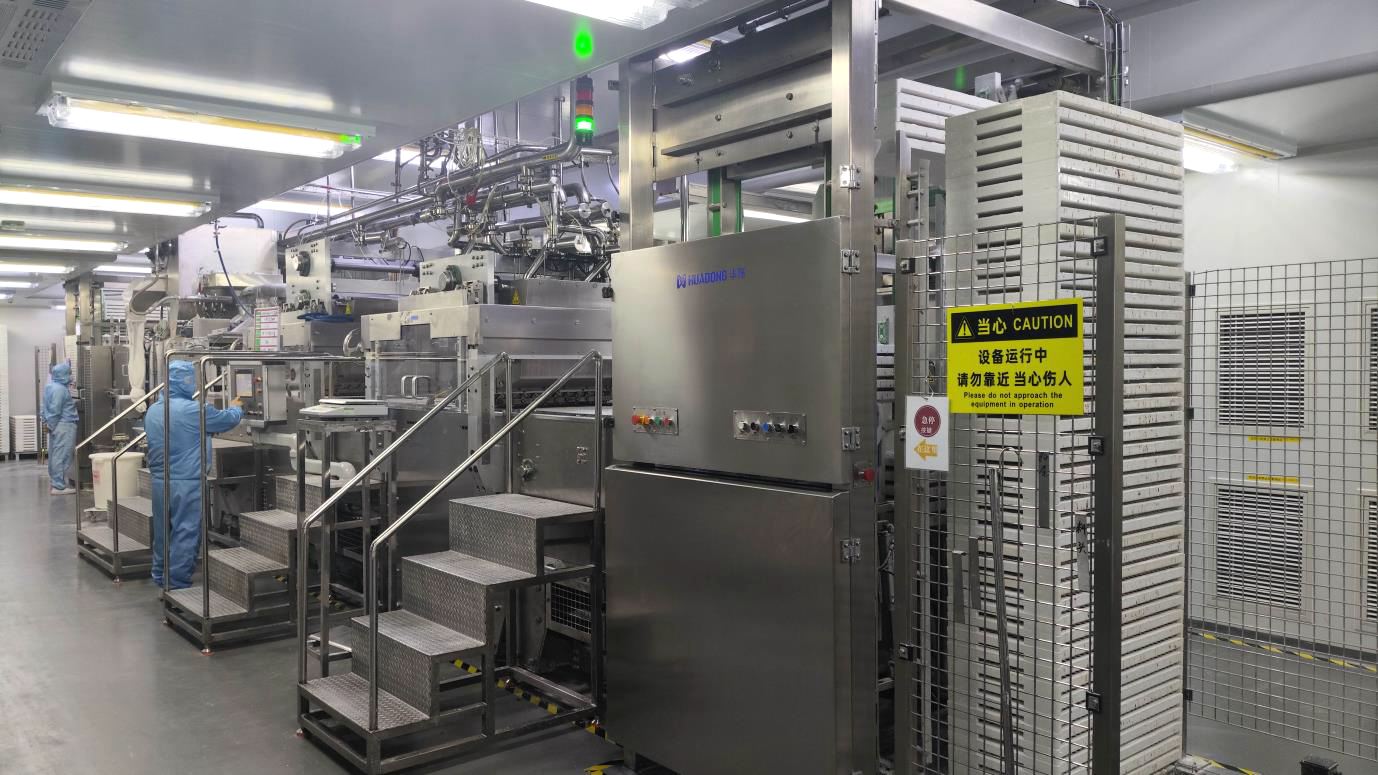
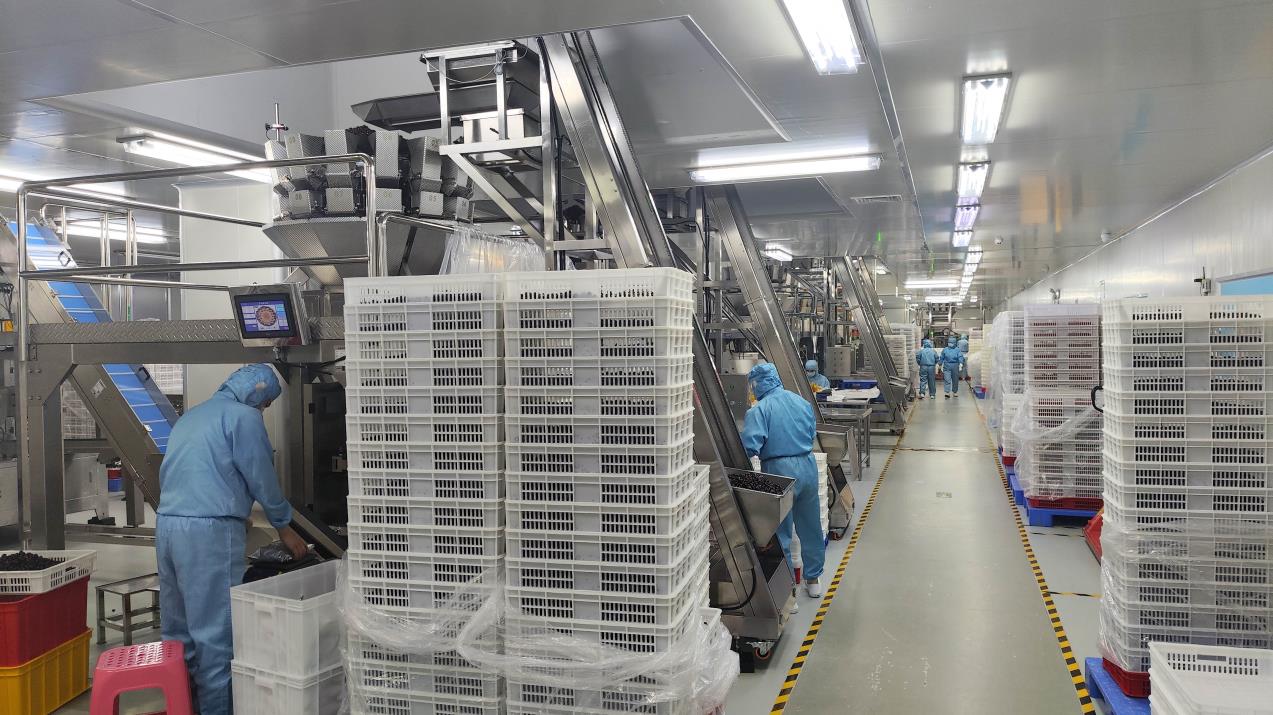
In the highly competitive dietary supplement market, time-to-market and supply chain cost efficiency are key differentiators. Manufacturing partners in China, particularly in developed industrial zones like Guangdong, offer significant structural advantages that go beyond lower labor costs.
Integrated Raw Material Sourcing: China is a leading global producer and processor of key botanical extracts, amino acids, vitamins, and active organic compounds. By locating manufacturing within this ecosystem, we minimize the transit time, oxidization risk, and freight costs of raw inputs. This allows us to source fresh ingredients directly, ensuring higher quality and potency for the final product.
Advanced Production Automation: Our facility utilizes advanced automated systems for dosing, mixing, encapsulation, and packaging. These closed-loop systems increase production speed and ensure batch-to-batch consistency by reducing human error. This automation allows us to offer flexible production scales, running large commercial batches alongside smaller runs to accommodate varying brand requirements.
Rapid Prototyping and Faster Turnaround: Our integrated operations allow us to provide pricing proposals within 24 to 48 hours and deliver pilot batches quickly. With standard lead times starting at 15 days, our partners can rapidly adjust to shifting market demands, seasonal trends, and new product opportunities.
We align our processing protocols with the requirements of major international markets. Our facilities maintain documentation ready for FDA registration, EFSA compliance, and Health Canada audits, ensuring smooth import customs clearances for our clients.
We work closely with clients to create customized formulations, offering adjustments to texture, natural color profiles, clean-label sweeteners, and targeted ingredient profiles to suit specific market segments and demographics.
We prioritize sustainable operations by sourcing ethically grown ingredients, using energy-efficient manufacturing processes, and offering eco-friendly, recyclable packaging materials to support our clients' environmental goals.
Nutraceutical brands face different consumer preferences and regulatory environments depending on their target region. Working with a versatile manufacturing partner helps brands adapt to these regional nuances.
North America: Consumers in this market heavily prioritize clean-label products, third-party testing transparency, and specific dietary certifications like Vegan, Non-GMO Project Verified, and USDA Organic. Popular product categories include zero-sugar hydration powders, active lifestyle supplements, and convenient, nutrient-dense formats like functional gummies.
Europe: The European market is characterized by strict European Food Safety Authority (EFSA) regulations regarding health claims and ingredient safety. Brands targeting this region often focus on minimal ingredient lists, eco-friendly packaging solutions, and science-backed formulations for gut health, cognitive function, and immune support.
Asia-Pacific: With a fast-growing, health-conscious middle class, the APAC region shows high demand for products addressing healthy aging, beauty-from-within (such as collagen peptides), and convenient single-serve packaging like stick-packs and liquid pouches that fit into busy, urban lifestyles.
We conduct comprehensive batch testing to verify raw materials and final product specifications. Our quality checks cover active ingredient density, heavy metal limits, pesticide residue screening, and microbiological counts to ensure compliance with global standards.
We work with established international freight forwarders to manage shipping logistics efficiently. We provide complete export documentation, including Bills of Lading, Certificates of Analysis, Phytosanitary Certificates, and Certificates of Origin.
Our formulation scientists collaborate with your R&D teams to refine ingredient profiles, resolve flavor challenges, and optimize stability, helping to ensure your products meet both taste preferences and efficacy goals.
Get quick, direct answers regarding our contract manufacturing processes, quality certifications, formulation support, and export logistics.
Explore our additional range of specialized formulations and performance supplements designed for health-conscious consumers.

 Eik Health